21.09.2026
Rotary Lobe Pump in the Food Industry: Hygienic and Efficient
The food and beverage industry places particularly high demands on conveying systems. Product safety and compliance with hygienic standards are not optional additions, but fundamental operational requirements enshrined in law. At the same time, delicate, textured or highly viscous materials must be conveyed gently and consistently, without any loss of quality or risk of contamination.
The rotary lobe pump has established itself as the solution of choice in numerous applications, particularly where centrifugal pumps reach their limits. We’ll show you how to ensure maximum process reliability whilst minimising cleaning requirements, thereby reducing your long-term operating costs.
How rotary lobe pumps work
Customised Consulting
Rotary lobe pumps belong to the group of rotary positive displacement pumps. Two counter-rotating lobe rotors, typically designed as two-, three- or multi-lobe units, create defined pumping chambers within the pump housing, which transport the fluid from the suction side to the discharge side without squeezing, shearing or crushing it.
This operating principle offers decisive advantages in food production:
- Preservation of structure: Chunky, fibrous or delicate products such as fruit, vegetable purées, meat or fish are conveyed gently, without altering their texture or appearance
- Viscosity tolerance: Rotary lobe pumps reliably convey media with highly variable or high viscosity, ranging from thin fruit drinks to creams, pastes and concentrates
- Low-pulsation conveyance: The uniform flow rate minimises mechanical stress on downstream plant components and enables stable process control
- Self-priming capability: The technology enables reliable priming even in difficult installation situations or at low inlet pressures
- Dosing accuracy: The defined displacement per revolution allows for precise flow control and facilitates integration into automated dosing and filling processes
Design requirements relevant for operation
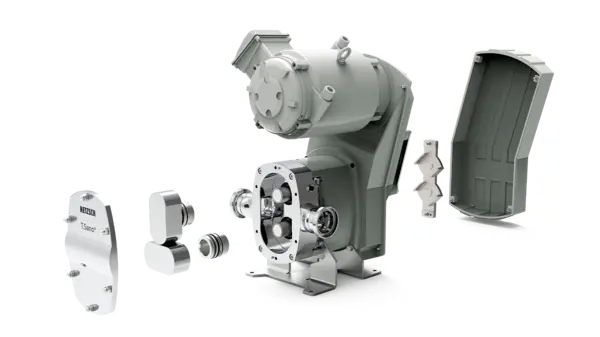
In the food industry, hygienic design is not a matter of aesthetics, but a design requirement directly impacting product safety and cleaning efficiency. Dead-space-free internal geometries, smooth surfaces without grooves or crevices, and ease of disassembly are key criteria for evaluating hygienic pumps. The TORNADO® rotary lobe pumps from NETZSCH Pumps & Systems meet these requirements and reliably comply with the standards of recognised certification institutions such as the EHEDG (European Hygienic Engineering & Design Group) as well as the material specifications of the FDA (U.S. Food and Drug Administration). The elastomers and sealing materials used are approved for food contact and can be individually tailored to specific media requirements, such as fatty, acidic, or alcohol-containing products. Furthermore, food-grade TORNADO® pumps from the global specialist in handling complex media are designed for CIP (Cleaning-in-Place) operation and, on request, also support SIP (Sterilisation-in-Place) processes. Cleaning cycles can thus be done without complete disassembly, significantly reducing your cleaning effort.
Applications in food and beverage production
TORNADO® rotary lobe pumps have a wide range of applications in the food industry. Typical pumping tasks range from fruit and vegetable purees and concentrates to dairy products such as yoghurt, quark and cream cheese and to seasonings, sauces, dressings and emulsified products. The TORNADO® is equally reliable at handling meat and fish in chunky or paste-like forms, chocolate and confectionery mixtures, as well as yeast, starter cultures and fermentation cultures. The technology is also widely used in animal feed and pet food production. The range of media to be conveyed – from low-viscosity to high-viscosity, from chunky to homogeneous – makes the rotary lobe pump a versatile solution in modern food production facilities.
Maintenance and availability: FSIP® as a factor of efficiency
Unplanned downtime in food production results in direct financial losses. Rapid response times for maintenance and servicing are therefore just as important as the pump’s reliability during normal operation. TORNADO® rotary lobe pumps stand out thanks to the innovative FSIP® (Full Service in Place) concept. This allows for complete maintenance and the replacement of all wear-prone components without removing the pump from the pipeline. Connections, seals and the pump’s positioning remain unchanged. Only the front of the pump is opened. This significantly reduces your maintenance effort, minimises downtime and lowers the requirements for tools and specialist personnel on site. Combined with NETZSCH’s global service network – including an emergency spare parts service and 24/7 availability – this results in a support framework tailored to the requirements of continuously operating plants.
Finding the right solution together
Selecting the ideal rotary lobe pump for a food processing application depends on a wide range of process-specific parameters: The medium, viscosity, temperature, flow rate, operating pressure, cleaning requirements and hygiene class are just some of the relevant factors.
The experts at NETZSCH will support you in designing and configuring the right solution. From the initial consultation and application analysis right through to commissioning and beyond. Working closely with you, we develop a pump solution that reliably meets your process requirements whilst ensuring cost-effective operation.